
Description
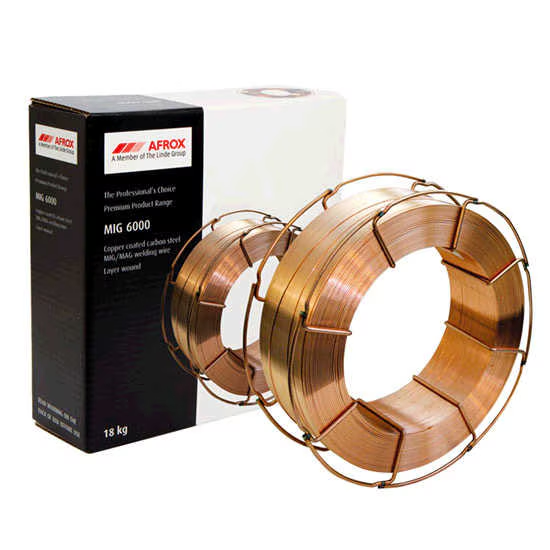
Afrox MIG 6000 is produced from high quality deoxidised rod.
The product is copper coated for increased shelf life, which facilitates good electrical conductivity and pick-up with reduced friction during high-speed welding.
MIG 6000 is a premium quality wire which is precision layer wound to provide positive uninterrupted feeding in semi-automatic and automated systems.
Welding Procedure
MIG 6000 is suitable for dip (short arc), spray arc and pulsed arc transfer welding using shielding gases such as Argoshield® 5, Argoshield® Light, Argoshield® Heavy and Argoshield® Universal as well as CO2. Gas flow rates of 15 l/min at low currents rising to 20 l/min at high currents should be used.
MIG 6000 Cert in 1,0 and 1,2 mm are tested in accordance with the requirements of AWS A5.01.
Classifications:
AWS A5.18 ER 70S-6
SABS 145 Grade A
EN ISO 14341 G42 2 C G4Si1
EN ISO 636-A W 42 3 W4Si1
EN ISO 636-B W 49 A 4 W4Si1
Approvals:
Lloyds Register of Shipping Grade DXVud,BF,2S,2YS,H15
American Bureau of Shipping Grade 2SA
South African Bureau of Standards
TÜV
Typical Chemical Analysis (All weld metal)
% Carbon 0,07 – 0,15
% Sulphur 0,035 max
% Manganese 1,4 – 1,85
% Phosphorous 0,03 max
% Silicon 0,8 – 1,15
% Copper 0,4 max (typical 0,18)
Typical Mechanical Properties (All weld metal in the as welded condition)
MIG 6000 with CO2 As Welded Stress Relieved Normalised
as Shielding Gas 650˚C/15 hr 920˚C/0,5 hr
0,2% Proof Stress 430 MPa min 360 MPa min 315 MPa min
Tensile Strength 510 – 570 MPa 490 – 570 MPa 470 – 550 MPa
% Elongation on 50 mm 26 min 26 min 26 min
Charpy V-Notch at +20˚C 110 J min 110 J min 80 J min
Charpy V-Notch at 0˚C 80 J min – –
Charpy V-Notch at -20˚C 47 J min 47 J min 47 J min


Reviews
There are no reviews yet.